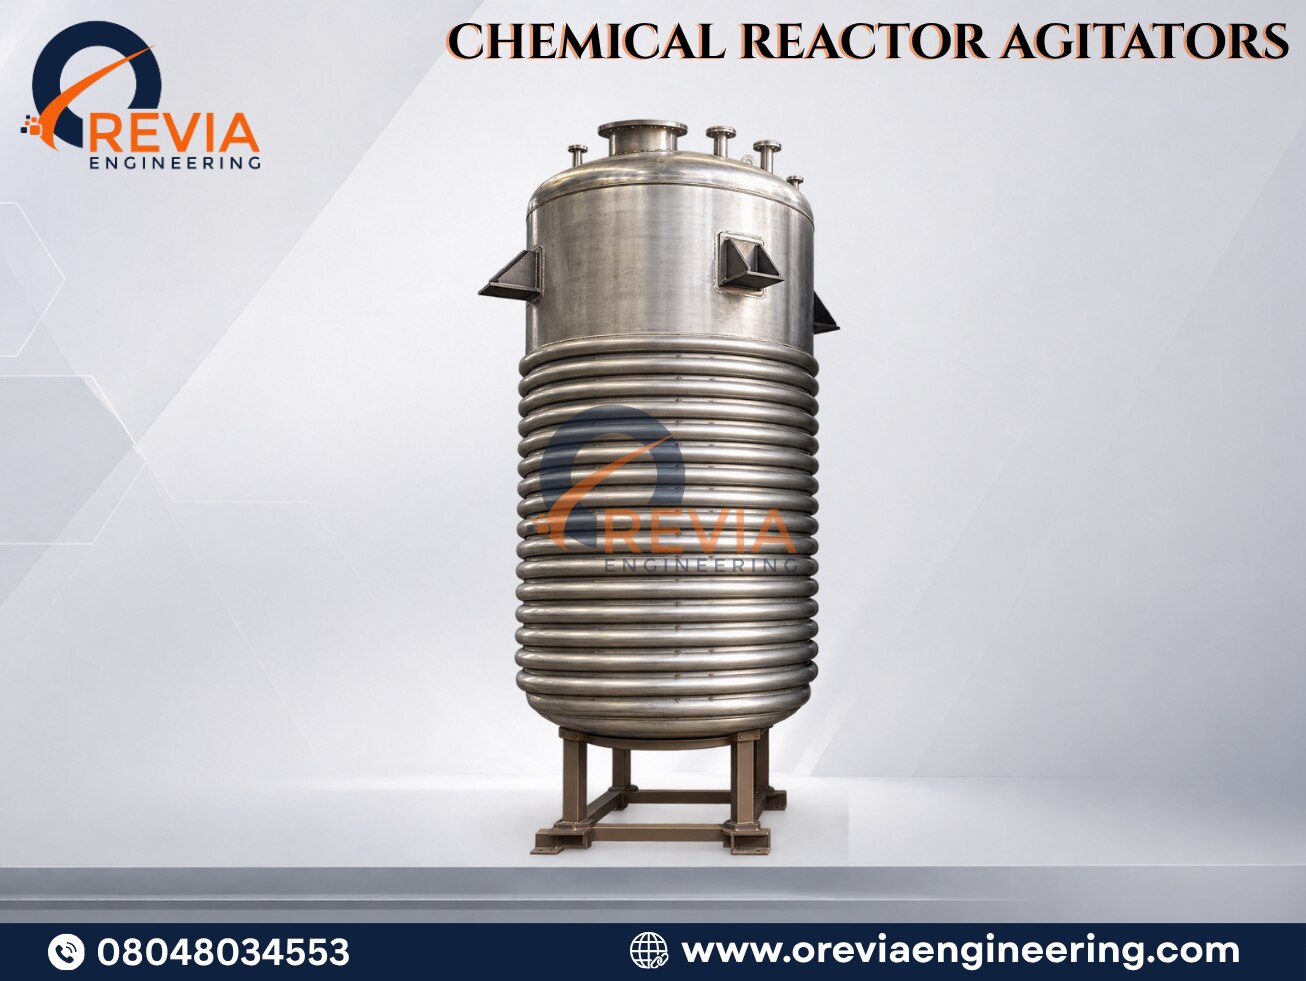
CHEMICAL REACTOR AGITATORS
Description
Chemical Reactor Agitators Manufacturer in Ahmedabad.
Efficient agitation is essential for achieving successful chemical processing and maintaining consistent product quality across industries such as specialty chemicals, polymers, pharmaceuticals, coatings, and industrial intermediates. A precision-engineered reactor agitator ensures uniform mixing, accurate temperature control, and improved reaction efficiency even in challenging production environments. At Orevia Engineering, we manufacture advanced Chemical Reactor Agitators designed to enhance productivity, reduce processing time, and deliver reliable performance. As a trusted Chemical Reactor Agitators Manufacturer in Ahmedabad, we provide customized agitation systems tailored to meet the specific requirements of modern chemical industries.
Chemical reactions often involve complex combinations of liquids, solids, gases, and high-viscosity materials that require controlled and continuous mixing. A well-designed Chemical Reactor Agitator promotes even distribution of reactants, improves reaction rates, and prevents issues such as sedimentation, separation, and uneven temperature zones. As a leading Chemical Reactor Agitators Supplier in Gujarat, Orevia Engineering develops customized solutions based on reactor capacity, material properties, operating conditions, and production needs, ensuring efficient processing and consistent results in every batch.
Technical Specifications
Our Chemical Reactor Agitators are manufactured using advanced engineering and premium-quality materials.
• Motor Power: Up to 100 kW
• Shaft Diameter: 30 mm to 300 mm
• Operating Temperature: -40°C to 200°C
• Operating Pressure: Full Vacuum to 10 Bar
• Impeller Types: Hydrofoil, Wide Foil, Turbine
• Shaft Sealing: Single Mechanical Seal, Double Mechanical Seal with Thermosyphon Pot
• Materials of Construction: Carbon Steel (CS), SS304, SS316, Duplex Stainless Steel, Super Duplex Stainless Steel, Alloy Materials
Every agitator is designed to deliver maximum performance while meeting stringent industrial quality standards.
Customized Agitator Solutions
Every chemical process has unique mixing requirements. Orevia Engineering manufactures reactor agitators specifically designed to match your application.
Our design considerations include:
• Reactor size and geometry
• Product viscosity and density
• Mixing intensity requirements
• Operating temperature and pressure
• Corrosive or abrasive process conditions
• Impeller configuration
• Shaft sealing requirements
• Material compatibility
As an experienced Chemical Reactor Agitators Distributor in India, we deliver customized solutions that improve operational efficiency while ensuring long-term reliability.
Benefits of High-Performance Chemical Reactor Agitators
Our reactor agitators are engineered to optimize every stage of the chemical manufacturing process.
Faster Reaction Rates
Efficient fluid circulation increases contact between reactants, improving reaction speed and conversion efficiency.
Superior Mass Transfer
Uniform mixing minimizes concentration gradients and enhances mass transfer, helping reduce unwanted by-products while improving overall product consistency.
Consistent Product Quality
Proper agitation eliminates dead zones inside the reactor, ensuring homogeneous mixing throughout the vessel for reliable batch-to-batch quality.
Enhanced Heat Transfer
Efficient circulation improves heat exchange between the reactor contents and vessel walls, allowing accurate temperature control during exothermic and endothermic reactions.
Applications Across Industries
Our Chemical Reactor Agitators are widely used in various industrial processes, including:
• Fine Chemicals & Specialty Chemicals
• Polymer Manufacturing
• Hydrogenation Processes
• Nitration Reactions
• Sulfonation Reactions
• Oxidation Processes
• Neutralization Systems
• Crystallization Processes
• Catalyst Mixing
• Distillation & Extraction
• Heat Transfer Applications
• Pharmaceutical Manufacturing
• Paint & Coating Industry
From laboratory-scale production to large industrial reactors, our agitation systems deliver consistent and dependable performance.
Engineered for Long-Term Performance
Orevia Engineering combines advanced design techniques with precision manufacturing to produce reliable reactor agitators for continuous industrial operation.
Key Features
• Optimized impeller design for superior mixing
• High-efficiency fluid circulation
• Excellent heat transfer performance
• Heavy-duty industrial construction
• Corrosion-resistant materials
• Low maintenance requirements
• High operational reliability
• Custom-built for specific process conditions
Our engineering team also utilizes advanced design principles to optimize flow patterns, improve mixing efficiency, and minimize energy consumption.
Why Choose Orevia Engineering?
Orevia Engineering has earned the trust of manufacturers by delivering innovative reactor agitation solutions that combine engineering excellence with exceptional durability. As a reliable Chemical Reactor Agitators Wholesaler in Gujarat, we provide customized equipment tailored to your process parameters, production capacity, and industry standards.
Our commitment to quality, innovation, and customer satisfaction ensures every solution is designed to improve productivity while reducing operational costs.
Need a customized Chemical Reactor Agitator for your manufacturing facility? Contact Orevia Engineering today for expert consultation and reliable industrial mixing solutions.
Frequently Asked Questions (FAQs)
1. What is the purpose of a Chemical Reactor Agitator?
A Chemical Reactor Agitator is used to mix liquids, solids, and gases inside a reactor vessel to improve reaction rates, enhance heat transfer, maintain uniform product consistency, and ensure efficient chemical processing.
2. Which industries use Chemical Reactor Agitators?
Chemical Reactor Agitators are widely used in chemical manufacturing, pharmaceuticals, polymers, paints, coatings, specialty chemicals, catalyst production, food processing, and other industrial processing applications.
3. Can Orevia Engineering customize Chemical Reactor Agitators?
Yes. Orevia Engineering manufactures fully customized Chemical Reactor Agitators based on reactor capacity, operating pressure, temperature, viscosity, impeller type, sealing system, and material of construction to meet your specific process requirements.