CENTRAL MIXER AGITATOR
Description
Central Mixer Agitator Manufacturer in Ahmedabad.
Efficient mixing plays a vital role in enhancing the performance of biogas plants and anaerobic digestion systems. Proper agitation helps maintain uniform slurry consistency, prevents sediment accumulation, and supports better microbial activity, resulting in improved biogas production. At Orevia Engineering, we manufacture high-performance Central Mixer Agitators designed specifically for large biogas digesters and industrial processing applications. As a trusted Central Mixer Agitator Manufacturer in Ahmedabad, we provide durable, energy-efficient, and customized mixing systems that ensure consistent digestion, higher gas yield, and reliable long-term operation.
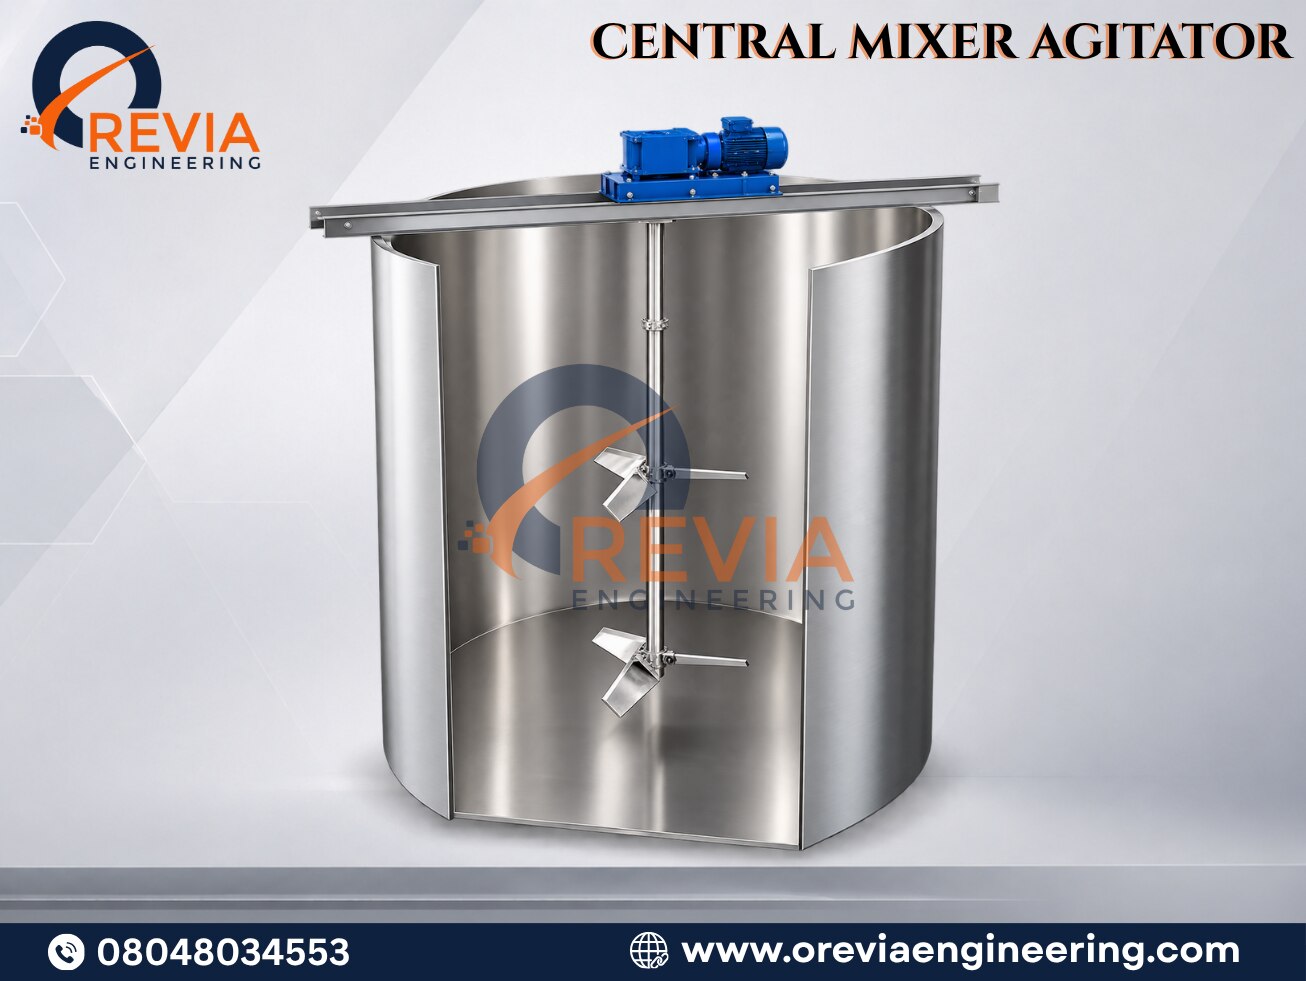
A Central Mixer Agitator is installed at the center of a digester tank to create effective vertical circulation and uniform mixing throughout the vessel. It continuously blends biomass, slurry, and organic waste to maintain proper microorganism distribution and stable digestion conditions. As a leading Central Mixer Agitator Supplier in Gujarat, Orevia Engineering designs precision-engineered agitators capable of handling challenging operating environments while delivering superior efficiency, durability, and consistent mixing performance for biogas and industrial applications.
Technical Specifications
Orevia Engineering manufactures central mixer agitators with specifications suitable for small and large biogas plants.
• Tank Capacity: 2,000 m³ to 10,500 m³
• Motor Rating: 11 kW to 55 kW
• Impeller Diameter: Up to 5.0 Meters
• Operating Speed: 10–30 RPM
• Shaft Length: Up to 20 Meters
• Material of Construction: Stainless Steel
• Power Supply: As per project requirements
Our systems are customized according to tank dimensions, feedstock characteristics, and operational requirements.
Key Features
Every Central Mixer Agitator is designed for reliable performance and long service life.
Product Highlights
• Suitable for high-viscosity feedstock up to 17% dry matter
• High-efficiency hydrofoil impeller design
• Gas-tight hydraulic shaft sealing system
• Heavy-duty helical gearbox
• Double taper roller bearings for extended durability
• Freely suspended shaft design
• Optional Variable Frequency Drive (VFD)
• PTC motor protection system
• CE, ATEX, IECEx, and PESO compliant options
• Corrosion-resistant stainless steel construction
As a reliable Central Mixer Agitator Distributor in India, Orevia Engineering ensures every unit undergoes strict quality testing before delivery.
Operational Benefits
Our Central Mixer Agitators help improve the overall efficiency of anaerobic digestion systems.
• Maximizes biogas production
• Uniform mixing throughout the digester
• Prevents sedimentation and floating crust formation
• Reduces maintenance and cleaning requirements
• Energy-efficient operation
• Longer equipment life
• Stable digestion process
• Improved plant productivity
These advantages help plant operators reduce operational costs while increasing energy output.
CFD-Based Design for Maximum Efficiency
Orevia Engineering utilizes advanced Computational Fluid Dynamics (CFD) analysis during the design process to optimize mixing performance.
CFD simulation allows our engineers to evaluate:
• Complete velocity distribution throughout the tank
• Efficient top-to-bottom circulation patterns
• Elimination of dead zones
• Uniform suspension of high-solid materials
• Optimized power consumption with maximum mixing efficiency
This engineering approach ensures every Central Mixer Agitator delivers superior performance under actual operating conditions.
Efficient Working Principle
Our Central Mixer Agitator uses strategically positioned impellers to maintain complete mixing throughout the digester.
Upper Impellers
The upper impellers continuously break floating crust layers, preventing blockage and improving contact between organic material and microorganisms.
Middle Impellers
The central impellers create strong bulk circulation, ensuring uniform movement of slurry throughout the digester.
Bottom Impellers
The lower impellers prevent sediment accumulation by keeping heavy particles suspended, reducing maintenance requirements and improving digestion efficiency.
Together, these impellers create a continuous top-to-bottom circulation loop that supports efficient anaerobic digestion and enhanced biogas production.
Applications
Our Central Mixer Agitators are widely used in:
• Biogas Plants
• Anaerobic Digesters
• Organic Waste Processing
• Agricultural Waste Treatment
• Industrial Wastewater Treatment
• Renewable Energy Projects
• Food Waste Digestion Plants
• Biomass Processing Facilities
Whether handling agricultural biomass or industrial organic waste, our agitators ensure efficient digestion and reliable operation.
Why Choose Orevia Engineering?
Orevia Engineering is dedicated to delivering innovative industrial mixing solutions that combine advanced engineering, reliable performance, and long-term operational efficiency. As a trusted Central Mixer Agitator Wholesaler in Gujarat, we provide customized equipment designed according to digester capacity, process requirements, and specific operational goals. With a strong focus on quality manufacturing, precision engineering, and customer satisfaction, we have become a preferred partner for industries across India seeking durable and efficient mixing solutions.
Looking for a customized Central Mixer Agitator for your biogas plant? Contact Orevia Engineering today for expert consultation and high-performance mixing solutions.
Frequently Asked Questions (FAQs)
1. What is a Central Mixer Agitator used for?
A Central Mixer Agitator is used in biogas digesters and anaerobic digestion systems to mix slurry, biomass, and organic waste uniformly, improving digestion efficiency and maximizing biogas production.
2. What industries use Central Mixer Agitators?
These agitators are commonly used in biogas plants, wastewater treatment facilities, renewable energy projects, agricultural waste processing, biomass plants, and organic waste management systems.
3. Can Orevia Engineering customize Central Mixer Agitators?
Yes. Orevia Engineering manufactures customized Central Mixer Agitators based on digester capacity, shaft length, motor power, impeller size, operating conditions, and project-specific requirements to ensure maximum performance and efficiency.